Equipment Behind Active's Metal Manufacturing
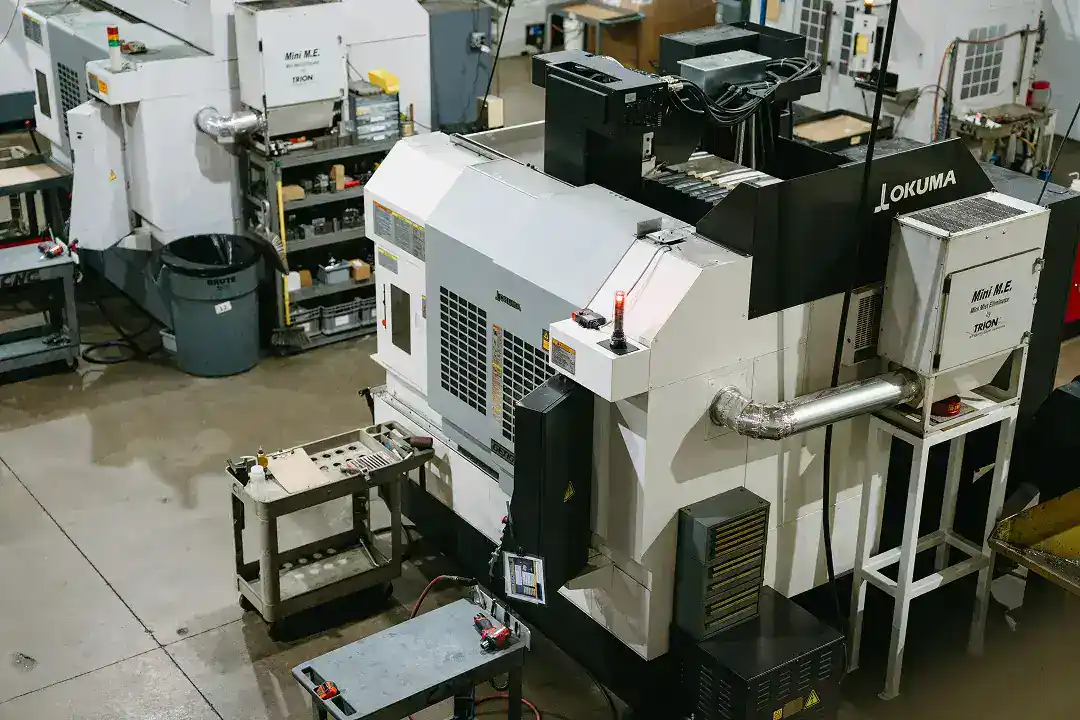
Active Manufacturing's equipment mix is built for difficult custom metal prototypes, short-run parts, and low-volume metal assemblies. The goal is not simply to own machines; it is to keep the right prototype manufacturing equipment available, staffed, and coordinated so engineers can move from design questions to manufacturable metal parts.
For a broader view of the shop environment, start with the metal manufacturing facility tour. If you already know the likely process path for your part, use this process-based equipment list to identify the relevant laser, press, EDM, CNC milling, welding, tooling, assembly, and inspection resources before requesting a quote.
U.S. Based
Proudly manufacturing in Michigan
Family Owned
Built on relationships. Focused on results.
ISO 9001:2015 Certified
Quality you can trust
ITAR Registered
Supporting defense and aerospace programs
How Active Uses Equipment for Prototype and Short-Run Work
Active's manufacturing capabilities are strongest when a part needs several processes coordinated through one team. A prototype may begin with laser cutting, move into forming, require welding or resistance welding, and finish with dimensional inspection. A short-run release may require stamping, EDM work, fixture support, assembly, and documented quality checks.
That coordinated approach supports production-intent prototypes, short-run releases, bridge production, difficult parts that conventional suppliers decline, and micro-to-larger metal components with process-sensitive features.
Laser
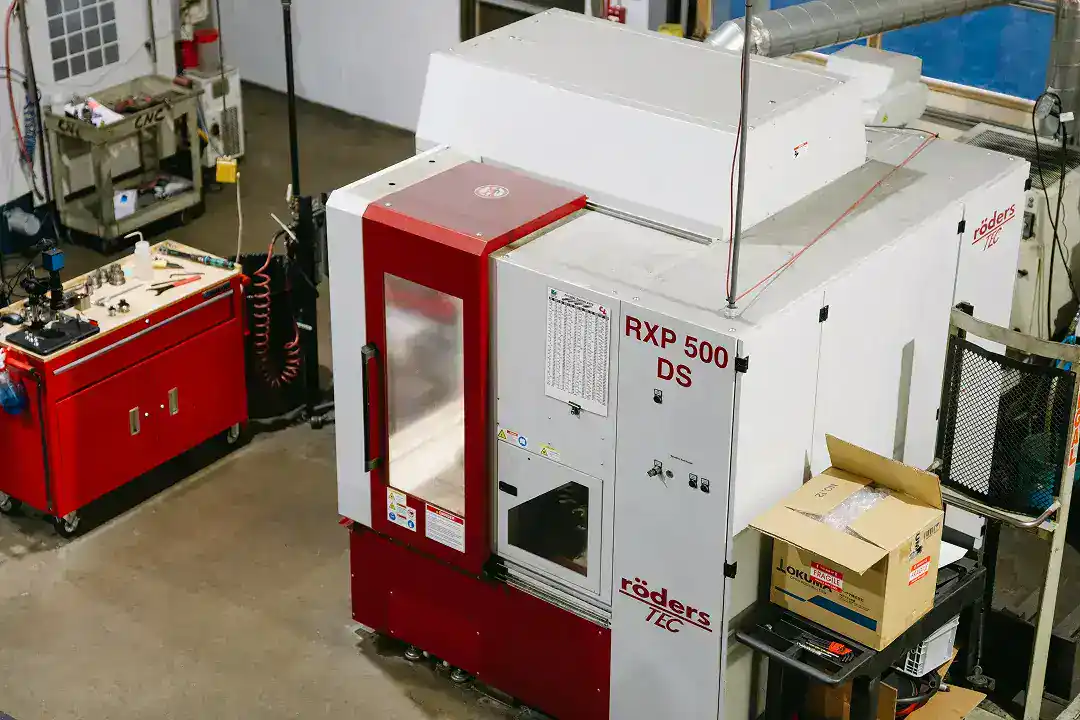
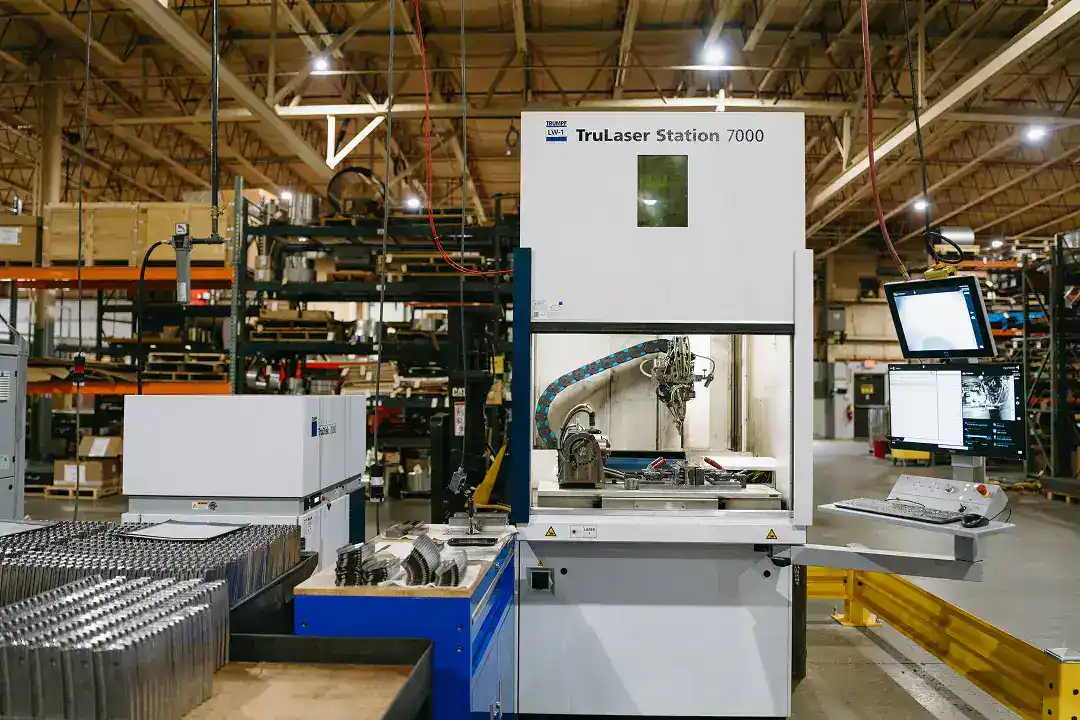
Active supports conventional laser cutting and fine-feature micro laser cutting. Conventional laser anchors include:
Material thickness from approximately 0.020 in to 0.375 in
A cutting bed up to 60 x 120 in
Tolerances of approximately +/-0.005 in or better, depending on the job
More Info
Micro laser cutting supports material from approximately 0.002 in to 0.020 in, work areas ranging from approximately 14 x 14 in to 36 x 40 in, and tolerances around +/-0.002 in depending on the part and material.
Prototype laser cutting capabilities
Micro laser cutting for fine-feature metal parts
Stamping and Forming Presses
Active's metal stamping presses and forming equipment supports:
Prototype metal stamping, micro forming, flat-spring and clip-style components
Tooling tryouts, and recurring short-run releases
Material down to approximately 0.001-0.002 in, (most work beginning around 0.003 in and thicker)
Press type, tonnage, tooling approach, material condition, geometry, and release quantity are reviewed for each part.
Precision metal stamping and forming
Micro metal components
Wire EDM and EDM Hole Drilling
Active's wire EDM and EDM hole-drilling equipment supports:
Precise profiles & fine holes
Tooling details, and conductive metal components that are not a fit for conventional cutting alone
EDM is often valuable when geometry, material hardness, or tolerance requirements make the process path more demanding
See wire EDM and EDM hole drilling for process fit, material considerations, and RFQ guidance.
Wire EDM and EDM hole drilling
CNC Milling Equipment
Active's multi-axis CNC milling equipment supports:
Prototype machining, low-volume machined parts, and tooling components
Fixtures, and precision metal features that complement stamping, laser cutting, welding, and assembly
Turning as a supporting capability
Active's primary machining emphasis is multi-axis CNC milling for prototype and short-run metal manufacturing.
CNC machining and milling page
Laser Welding, Resistance Welding, and Assembly Equipment
Active's joining resources include:
For joining-focused projects, review laser welding and micro welding or metal assemblies and secondary operations.
Laser welding and micro welding
Metal assemblies and secondary operations
Tool Room and Process Support
Active's tool room supports:
fixture development & tooling adjustments
Process troubleshooting, and production-intent setup support
Manual machining, cutting, and grinding
Visit tooling, fixtures, and process development for related capabilities.
Tooling, fixtures, and process development
Quality Inspection Equipment
Active uses:
Coordinate measuring, vision and optical inspection, laser profiling, comparators
Load and hardness testing
Camera or microscope inspection as appropriate for the parts it manufactures
Inspection is part of Active's manufacturing and quality-control workflow. Active does not offer a standalone third-party inspection bureau.
Inspection and quality control
Quality, certifications, and compliance
Multiple Processes. One Team. Manufacturable Results.
From lasers and presses to EDM, CNC milling, welding, and inspection, our equipment and people work together to deliver production-intent prototypes and short-run metal parts—on time and on spec.
Equipment FAQs
Which equipment is used for prototype and short-run projects?
Active may use laser cutting equipment, metal stamping presses, wire EDM and EDM hole-drilling equipment, CNC milling equipment, welding and assembly resources, tooling support, and quality inspection equipment depending on the part.
Can multiple equipment categories be combined for one part?
Yes. Many best-fit projects use multiple coordinated processes, such as laser cutting, forming, welding, machining, EDM, and inspection.
What part sizes and tolerances can the equipment support?
Confirmed conventional laser anchors include approximately 0.020 in to 0.375 in material thickness, a 60 x 120 in bed, and approximately +/-0.005 in or better depending on the job. Micro laser cutting supports approximately 0.002 in to 0.020 in material, work areas from approximately 14 x 14 in to 36 x 40 in, and tolerances around +/-0.002 in. Final capability depends on the full RFQ.
How are machine capabilities verified during an RFQ review?
Active reviews the drawing, material, quantity, geometry, tolerance requirements, finishing needs, timing, and compliance requirements before confirming the recommended process path. If an exact machine specification matters, identify it with the RFQ so the current equipment match can be verified.
Ready to confirm the right process for your part?
Submit a custom metal parts quote with your drawing, material, quantity, and timing notes.
Equipment Fit Is Confirmed During RFQ Review
The best machine path depends on material, thickness, tolerances, geometry, quantity, finish needs, and whether the work involves controlled or confidential files. Active reviews each RFQ to determine which equipment categories should be used and whether several processes need to be combined.
Exact makes, models, machine counts, work envelopes, and current availability should be confirmed with Active when a specific machine requirement affects the project. To help the team evaluate fit, include drawings or CAD files, material, quantity, critical features, and timing. If controlled files are involved, do not upload them through the ordinary public form; request secure-transfer coordination instead.